 Related
Automatic bottle rinsers
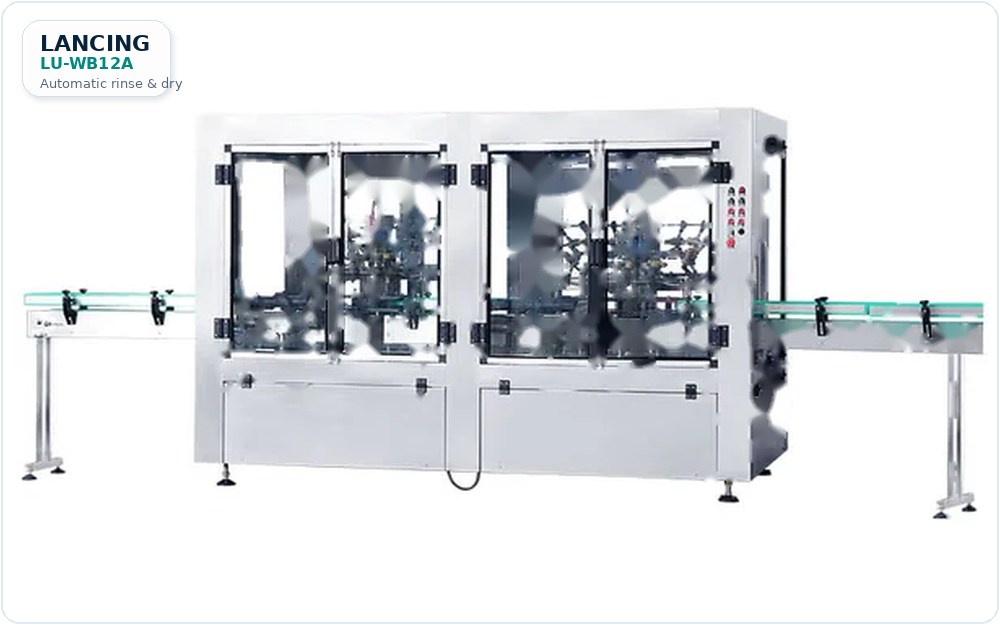
Inline machines for higher-output lines.
Explore route →Bottle rinser maintenance guide covering nozzles, filters, pumps, air quality, drainage, guarding and operator checks.
This guide focuses on bottle rinser maintenance. The best answer depends on the exact bottle format, the reason for rinsing, the target output and the line equipment around the rinser. A bottle rinser that works well in one line can struggle if the bottle is lighter, taller, unstable or needs a different rinse method.
For operators and production managers, the most useful first step is to separate three questions: what has to be removed, whether the bottle may get wet, and how quickly the bottle needs to leave the rinser and enter the filler.
The most common mistake is choosing by price or machine name before proving the bottle handling. Routine checks, cleaning schedules and spares planning can change the specification because stability, bottle opening, rinse dwell time and conveyor transfer all affect real production performance.
Another common issue is ignoring the downstream equipment. The rinser must not only clean the bottle; it must present it to the filler, capper or labeller at a speed and condition that the rest of the line can accept.
Send bottle dimensions, photos, target output and a short description of the current line. Lancing can then compare maintenance planning against the bottle and line constraints before suggesting the most suitable bottle rinsing route.
These checks help match the rinser to the bottle, line speed and filling environment.
| Check | Why it matters | Send with enquiry |
|---|---|---|
| Bottle format | Shape, weight and neck finish affect stability, access and change parts. | Photos, drawings or samples |
| Rinse method | Air, water and rinse-dry routes need different utilities and machine layouts. | Cleaning requirement and contamination risk |
| Output target | The rinser must keep pace with the filler without starving or flooding the line. | Bottles/minute or bottles/hour |
| Integration | Conveyor height, space and downstream transfer can decide the practical route. | Line photos or layout sketch |
RelatedInline machines for higher-output lines.
Explore route →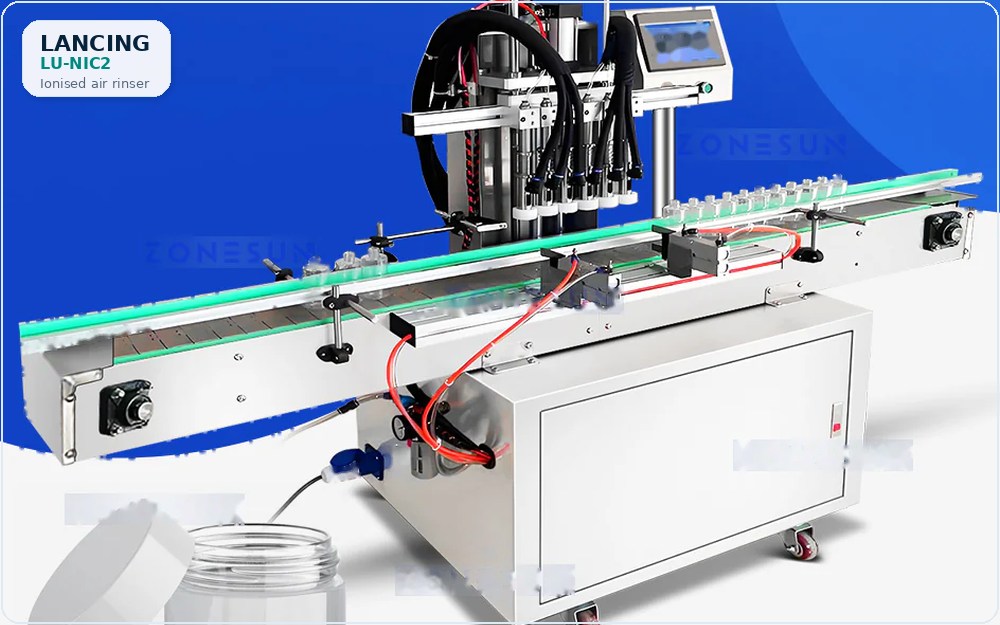 Related
Dry bottle cleaning before filling.
Explore route → Related
Get specification support for your line.
Explore route →Bottle rinser maintenance affects machine selection because the rinser has to match the bottle, required cleanliness, utilities, output and filling line layout.
Send bottle photos, dimensions, material, neck finish, target speed, available utilities and details of the filler, capper or labeller connected to the line.
Yes. The enquiry can be reviewed against the bottle format, line speed, utilities and integration details before a practical shortlist is suggested.
Maintenance planning is part of specification. Operators need access to inspect nozzles, clean drain areas, adjust guides, check filters and replace change parts without dismantling the line unnecessarily.
| Check | How to validate it | Why it affects specification |
|---|---|---|
| Nozzles | Check removal, inspection and alignment method. | Maintains consistent rinse contact. |
| Filters and air/water services | Define routine inspection points. | Protects rinse quality. |
| Guides and change parts | Label and store format parts clearly. | Reduces changeover errors. |
| Drain areas | Make cleaning and inspection practical. | Prevents debris build-up. |
Maintenance should not finish when a component has been replaced. Before the rinser returns to production, confirm that tools and loose parts are removed, guards and interlocks are restored, utilities are reconnected correctly, nozzles and filters are fitted in the approved orientation, drains or extraction are clear, and the selected bottle format passes a first-off check.
HSE guidance on work equipment states that machinery should be maintained in an efficient state and that maintenance operations must be carried out safely. It also emphasises planning, competence, safe isolation and control of stored energy. The site's risk assessment and the machine manufacturer's instructions remain the authority for the actual task; a general bottle-rinser checklist cannot replace them.
The pre-start and changeover checklist gives a structured production-release record. The filtration guide covers filter condition, drains and point-of-use records.
Closing the maintenance task does not automatically prove that nozzle alignment, holder position, utility integrity, controls or rinse performance remain inside the approved condition. Use a risk-based check after work that can affect the bottle path, rinse medium or safety function.
Record the work, parts, settings and inspection, then run first-off or targeted samples. Significant changes should follow the revalidation and change-control guide.